
Watch movement component polishing follows a different rule set from general hardware finishing. Mainplates, bridges, train wheels, pinions, and balance parts carry dimensions measured in microns, and a standard deburring recipe can round a pivot shoulder, pack a jewel hole, or destroy the flatness that keeps the escapement running. Shops that struggle with movement components are rarely using the wrong machine; they are applying general finishing logic to parts that need controlled micro precision finishing. The right process protects critical geometry while still producing a clean, uniform surface, and it starts with media size, energy level, and a part-specific recipe rather than a higher speed.
Why Does Watch Movement Component Polishing Need a Different Process?
Most standard finishing cycles fail on movement components because of uncontrolled media contact. A 2 mm ceramic triangle removes burrs efficiently on a brass faucet body, but that same media acts as a wedge inside a 0.8 mm hole or across a pinion leaf. When media packs into a confined space, it can peen hole walls, roll an edge, or trap abrasive in a pivot bearing even after washing.
Flatness is the second issue. Thin mainplates and bridges flex under high mass finishing energy. A part that arrives with a clean edge but a bowed reference surface may pass visual inspection and fail later at assembly because the gear train no longer sits on a single plane. We have seen movement plates that looked polished but had lost 0.002 mm of flatness because the bowl was overloaded and the parts rode against each other.
A controlled recipe changes the objective from heavy removal to selective surface refinement. The goal is to break sharp corners, remove micro burrs, and improve surface texture without changing functional form. That distinction drives every machine and media choice that follows.
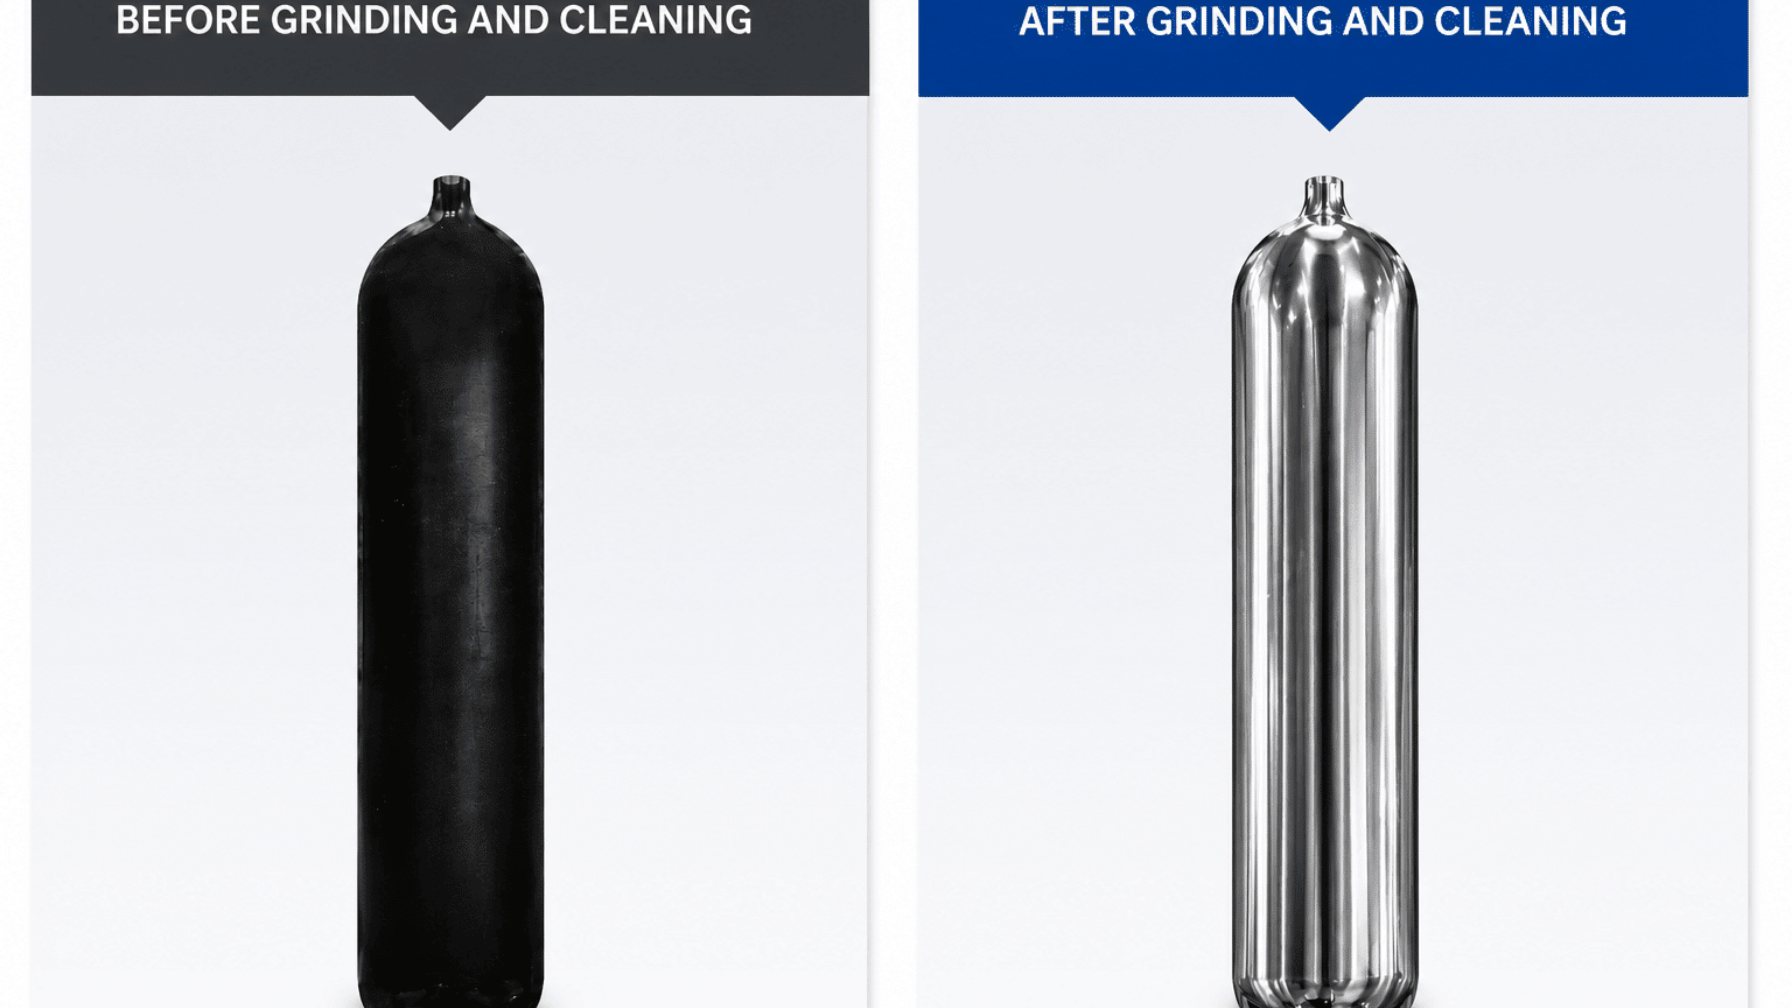
Which Machines and Media Fit Micro Precision Components?
The machine choice starts with the feature that is hardest to protect. For flat bridges, mainplates, and levers, precision centrifugal disc finishing offers the best combination of energy and gap control. The PD series runs with a 0.15 mm adjustable gap, and the CF series brings the dry gap down to 0.05 mm. For pinions, small holes, and blind recesses, magnetic finishing reaches areas a solid media cannot enter.
| Process | Best fit in movement parts | Key control factor | Typical media | Main risk |
|---|---|---|---|---|
| Precision centrifugal disc | Flat bridges, mainplates, levers | 0.05 to 0.15 mm disc gap | Fine porcelain pins, small ceramic shapes | Edge roll if gap is too wide |
| Magnetic finishing | Pinions, small holes, blind recesses | Magnetic pin diameter between 0.1 and 1.0 mm | Stainless steel magnetic pins | Media entrapment if pins are too long |
| Drag finishing | Pivots, arbors, fixtured parts | Fixture orientation and drag depth | Fine walnut shell or porcelain media | High setup labor |
| Small vibratory bowl | Open pre-deburr work | Media to part ratio and fill level | Light cut plastic media | Media jamming in small holes |
| Centrifugal barrel EB | Heavy burr removal before precision stage | Barrel speed and fill level | Small ceramic or steel media | Too aggressive for final finish |
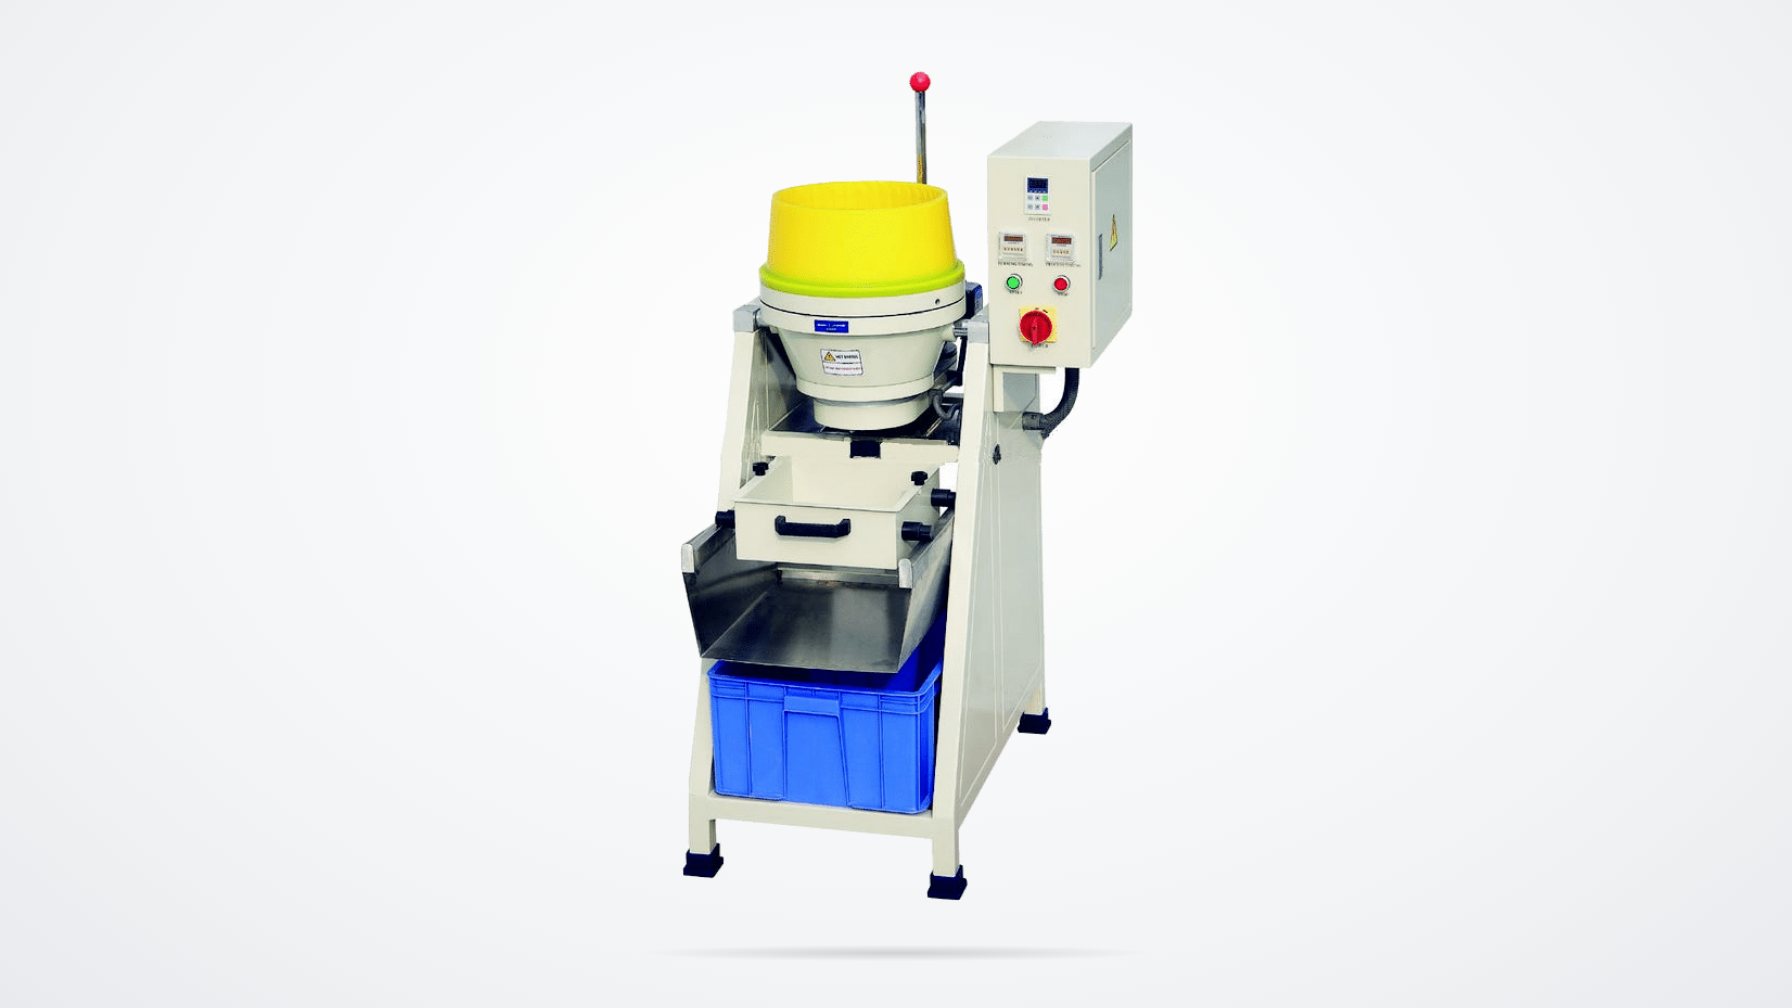
When the priority is a flat surface and a controlled edge break on small precision parts, high precision disc finishing is usually the most direct route. <Top Centrifugal Disc Finishing Machines for High Efficiency Surface Treatment> covers how disc speed, gap setting, and media selection work together for high energy finishing on small components.
Why is media size more important than machine speed for movement parts?
Media size sets the minimum radius the process can reach. If the media is larger than the feature, it either skips the feature or wedges into it. For a 0.5 mm slot, we look for media with a diameter below one-third of the slot width. Speed and energy then change removal rate, but they cannot correct a geometry mismatch. Most movement part scrap we see comes from media that is too large, not from finishing time that is too short.
When does magnetic finishing outperform centrifugal disc finishing?
Use magnetic finishing when the critical surface is inside a hole, slot, or recess that a disc media cannot reach. Stainless steel pins from 0.1 to 1.0 mm in diameter move through the magnetic field and contact internal features without high part-on-part pressure. For flat plates and bridges, disc finishing is faster and easier to unload. For pinions, jewel holes, and balance cocks with blind features, magnetic pins reduce the risk of leaving untreated burrs in dead corners. The two processes are often adjacent steps rather than competing options.
Which Process Parameters Protect Critical Dimensions?
The first parameter to lock is fill level and media to part ratio. Overloading a bowl drives part-on-part contact and flattens fine features. We prefer a ratio that keeps parts separated by at least two or three media layers, but not so high that the mass becomes sluggish.
The second parameter is water or compound flow. For brass and steel parts, a light cleaning compound carries swarf out of the gap and prevents abrasive from building up on flat surfaces. Too much liquid floods the mass and reduces contact; too little lets swarf load. We adjust flow until the media surfaces stay damp and the parts come out clean, not coated.
What surface roughness is realistic for ground and polished watch parts?
After a pre-grind or light deburr step, a precision disc or magnetic finishing stage can take flat brass or steel components to a bright surface in the Ra 0.1 to Ra 0.2 µm range. Reaching below Ra 0.1 µm typically requires a finer porcelain or zirconia media stage and careful compound control. The realistic number depends on the starting surface; if the blank arrives with deep tool marks, the first step is cutting, not polishing. Buyers should ask for a test run on their own parts rather than accepting a generic Ra figure.
How do you keep small holes and slots from packing with media?
The simplest fix is media size. For a hole that must stay open during processing, choose media with a diameter large enough that it cannot enter the hole, or fine enough to rinse out cleanly. For blind holes, size alone is not enough; the process should use magnetic pins or a fixture that orients the part so the hole does not face the media flow. We also avoid mixed media sizes with long, thin shapes because they bridge slots and lock together under vibration.
Even with the right machine category, the load layout and gap setting should be checked before you commit. If the parts fall below 2 mm or include blind holes and thin flexures, send a part drawing and batch quantity to Mass Polishing through the website inquiry form. We will confirm the process window against the geometry before you build a finishing line.
What Failure Modes Should You Check Before Scaling Up?
Edge roll is the most common failure. It happens when a sharp edge receives more energy than the material can hold, so instead of breaking the burr the process folds it over. We look for edge roll first on gear teeth and pinion leaves. If the edge profile is shiny and rounded under 10x magnification, the cycle is too aggressive; reduce speed or switch to a finer media before the feature loses form.
Media entrapment is the second failure. Small triangular media can enter a hole during the vibration stroke and seat inside. When the part moves to the next station, the media may not be visible, but it will interfere with assembly or appear later as contamination. We check holes under magnification after a short test cycle, not after the full batch.
Flatness loss is the easiest to miss. A bridge may look polished under normal light but still be bowed if it was processed with too much part-on-part pressure. We test flatness on a granite plate with a dial indicator before and after a short batch; if the reading changes more than the print tolerance, the load configuration is wrong.
Cross contamination also matters. Steel pins and brass parts do not mix well. If the same machine runs steel components with magnetic pins, the pins can carry iron residue into a brass or gold plated batch and cause staining. We reserve media and compounds per material group when the finish is critical.
What Should You Confirm Before Committing to a Finishing Line?
Many watch component programs look simple on paper and become difficult when the first pilot batch arrives with polished faces but worn pivot shoulders. The difference is rarely the machine brand; it is whether the process was developed around the part geometry and acceptance criteria.
A practical next step is to send the part drawing, material grade, current surface condition, target Ra, and monthly volume. Mass Polishing’s engineering team reviews the part profile against the right machine and media combination, then runs a sample process before quoting production equipment. Submit the drawing and batch data through the contact form at www.masspolishing.com.
What Do Buyers Ask About Watch Movement Component Polishing?
Can movement components be batch polished without losing dimensional accuracy?
Yes, when the cycle is built around the smallest critical feature rather than the average part size. Start with the pivot diameter, jewel hole, slot width, or leaf spacing that has the tightest tolerance, and choose media that cannot enter or bridge that feature. Run a short cycle first, inspect under magnification, and only then scale up. Dimensional loss usually comes from part-on-part contact or oversized media, not from the polishing action itself. With a controlled load and a fine media stage, movement parts can be batch finished without measurable change to functional dimensions.
What surface finish can a precision disc or magnetic cycle achieve?
It depends on the starting surface and the final inspection standard. If a brass or steel blank arrives with fine tool marks, a cutting stage first removes the machining lines, then a precision disc or magnetic finishing stage can take flat surfaces into the Ra 0.1 to Ra 0.2 µm range. Mirror finishes below Ra 0.1 µm require finer porcelain or zirconia media and tighter compound control. The realistic target changes with geometry; recessed areas and inside corners do not refine at the same rate as flat surfaces, so ask for a pilot run on your own parts rather than a generic number.
Is magnetic pin finishing safe for jewels and assembled parts?
A common assumption is that magnetic finishing means dropping a complete movement into the machine. That is not how production finishing works. Magnetic pins are used on individual steel or brass components such as pinions, levers, and bridges, before assembly and before jewels are pressed in. The pins can reach blind holes and narrow slots, but they are not intended for assembled movements with jewels, shock springs, and lubricants. For assembled parts, the safer approach is a gentle cleaning or polishing method that does not involve free media. Process development should always start with the component, not the assembled caliber.
How long does a movement component finishing cycle take?
In the small part programs we run, a precision finishing stage commonly takes 15 to 45 minutes, but cutting before polish can add another hour depending on the burr condition. Magnetic finishing runs shorter, often 10 to 30 minutes, because the pins are light and the action is localized. The total cycle time matters less than the staged sequence: cutting, refining, then cleaning and drying. We usually quote cycle time only after a sample run because the same part name can vary widely between suppliers in raw burr and surface condition.
What should I send for a process test?
The more useful question is not whether the part can be polished, but whether the process can hold the functional features while the surface improves. Send the part drawing with material grade, critical dimensions, current surface roughness or a reference sample, target finish, and monthly volume. Also note any plating, coating, or assembly step that follows because that changes the required surface. With those inputs we can narrow the machine and media selection, run a test batch, and confirm the cycle before you buy. Share your part number and batch size with Mass Polishing, and we will confirm the right machine and media combination for your line.
If you’re interested, check out these related articles:
Aerospace Industry
The Vibratory Tumbler Explained
Ceramic Polishing Media Complete User Guide
Cutlery Manufacturers