
Precision deburring and edge breaking for aerospace parts covers two requirements that are usually written as one: removing the burr a cutting tool left at the edge, and producing the edge condition the drawing actually specifies. The first is a cleanliness check. The second is a dimensional and surface requirement, measured like any other callout, and it is where rework often starts. A part can pass a visual burr inspection and still fail its edge specification, because a hand-filed edge that looks clean can be under-broken in one place and rolled over in another. What follows deals with how the requirement is defined, which process can hold it, and how to prove the process before it runs on production parts.
What an Aerospace Drawing Actually Asks For at the Edge
Machined edges arrive with a burr because the last pass does not cut cleanly through the corner. The tool pushes a thin lip of material ahead of it, and that lip stays attached. How much stays attached depends on the alloy, the tool geometry, the feed rate, and how sharp the tool was on the final part of the run. A deburring operation removes that lip. It does not automatically produce a controlled edge.
Drawings describe the required end state in ways that carry very different acceptance criteria:
- “Break sharp edges” states an intent, not a measurement. Two inspectors can look at the same part and disagree.
- A specified radius, for example 0.2 to 0.4 mm, is a measurable callout and needs a measurement method agreed in advance.
- “Burr-free” is usually a visual or tactile criterion, and it says nothing about the radius.
- A general note pointing to a customer process specification pulls in a document the shop may not have read.
The distinction matters because the three conditions can exist independently. An edge can be free of burrs and still sit outside the radius callout. An edge can carry the right radius and still hold a folded lip of metal pressed into the corner, which is what happens when a burnishing step is used where a cutting step was needed. An edge can also look acceptable at the bench and fail at coating, because a corner that has been rolled over presents a different surface to the pretreatment line than a corner that has been cut back.
Before choosing a process, settle four things in writing: the radius or chamfer value with its tolerance, the measurement method the customer accepts, the surfaces that are excluded (threads, seal faces, bearing seats, datum edges), and whether the requirement applies to every edge on the part or only to the edges named on the drawing. That last point causes more disagreements than the radius value itself, because a general note is easy to read differently on a part with two hundred edges.
Why Aerospace Edges Behave Differently From Commercial Parts
Material behavior drives most of the difference. Aluminum smears rather than cuts under light pressure, so a burr can be folded back and forth instead of removed, and soft alloys mark easily when media pressure is uneven. Titanium work-hardens at the surface, and the layer the tool leaves behind is not the same as the base metal, so a finishing step that only polishes can leave a hardened lip in place. Nickel-based alloys such as Inconel are abrasive and work-harden quickly, which shortens media life and changes the cut rate as the charge wears.
Titanium is one of the alloys where the finishing sequence matters more than the finishing pressure. <How to Polish Titanium Parts a Step By Step Guide> covers a step-by-step approach to polishing titanium parts.
Geometry adds a second set of problems. Thin walls and long unsupported sections flex under media load, and a part that vibrates in a bowl is being finished under conditions nobody specified. Internal intersections, cross-holes and slots create burrs that loose media cannot always reach, and the same features trap media that then has to be found and removed. On a commercial part, a trapped media particle is an inconvenience. On a part that enters an assembly with a cleanliness requirement, it is a nonconformance.
Value changes the risk calculation. When one part carries a large share of the finished assembly cost, a process that usually holds the edge but occasionally over-breaks a corner is a poor trade, even if its average cycle is faster. That is why fixture-based processes stay in aerospace work despite lower throughput.
There is also the question of what the finishing step does to the surface it inherits. Mass finishing removes material at the edge and, to a lesser degree, across the surface. Where the machining process was qualified with a specific surface condition, the finishing step has to sit inside that qualification rather than being applied afterwards as a cosmetic operation.
Matching the Finishing Process to the Part
Six process families cover most aerospace edge work. They differ in how the media reaches the edge, how much control the operator has over the radius, and what can go wrong.
| Process | How the media reaches the edge | Edge character | Watch for |
|---|---|---|---|
| Vibratory bowl, SW and SWS series | Loose parts and media in a urethane-lined bowl | General burr removal with a blended radius, moderate control | Part-on-part contact, media lodged in holes |
| Centrifugal disc, ED and CF series | Media and parts pressed against a rotating disc wall | Fast cutting, radius set by media size and gap | Over-broken thin edges, smearing on soft alloys |
| Centrifugal barrel, EB series | Four barrels on a rotating turret | Short cycles, uniform radius, fine finish possible | Barrel size limit, load and unload labor |
| Drag finishing, DF series | Each part held in a fixture and dragged through the drum | Per-part edge control, leading edges protected | Fixture cost per part number, lower throughput |
| Magnetic finishing, MF series | Steel pins driven by a magnetic field | Reaches bores, slots and intersections loose media misses | Small features only, pin size limits |
| Trough vibratory, TV series | Long or large parts in a U-shaped vibrating tub | Gentle treatment of long edges | Slow cycle, limited radius control |
Machine – Deburring & Separation)
The choice usually follows the acceptance criterion rather than the part size. If the drawing calls a radius with a tolerance on a high-value part, the process has to hold that radius repeatably, which points toward a fixture-based method or a high-energy barrel run with a fixed recipe. If the requirement is burr removal on a high-volume small part under a general note, a bowl or disc machine is usually cheaper, and the spread of radius across the batch matters less.
Combinations are common and often better than a single step. A rough cut in a vibratory bowl removes the bulk of the burr and blends the edge, then a shorter high-energy run or a drag pass brings the radius into the window and improves the surface. Splitting the work lets each step run with media matched to its job instead of compromising on one media that does both jobs poorly.
Process)
High-energy processes earn their place where cycle time is the constraint. The published specification for the ED series states that these machines deliver 10 to 15 times the force of a conventional vibratory system. That figure describes working force at the bowl wall, not an edge result: the radius still comes from media size, media condition and time in the machine, and a high-force process with the wrong media will over-break a thin edge faster than a gentle one.
Machine – High Energy Deburring)
Barrel capacity sets a practical limit that is easy to overlook. The EB 240, for example, runs four 60 L barrels at up to 105 rpm on an 11 kW drive, and the EB 320 runs four 80 L barrels at up to 90 rpm. Those envelopes suit brackets, fasteners and small machined components. A long structural section does not fit, and forcing it into a barrel with fewer parts to fill the volume changes the part-to-media ratio and therefore the result.
Barrel machines are often judged on cycle time alone, when the more useful question is what the barrel does to the edge across a batch. <What Are the Characteristics of a Centrifugal Barrel Finishing Machine> covers the characteristics that separate centrifugal barrel finishing from other mass finishing methods.
Where mass finishing cannot reach, say so early. A burr at the intersection of two cross-holes in a deep bore may need a directed-flow process, a pin-based method, or a manual touch that is then controlled by a written standard. Planning for that secondary operation is cheaper than discovering it during first article inspection.
Media and Compound Choices That Set the Edge Radius
A loose-media process produces the edge radius through many small contacts. The practical ceiling on the radius is set by the largest media contact that can physically reach the edge, which makes media size the first decision and media material the second. Coarse media cuts quickly and leaves a larger, less controlled radius. Fine media follows the edge more closely and produces a smaller radius with a better surface, at the cost of cycle time.
| Media class | Action at the edge | Typical aerospace use | Limit |
|---|---|---|---|
| Coarse ceramic, TC to UC | Cuts fast and sets a larger radius | Deburring after milling, radius blending | Matte surface, radius can overshoot on thin edges |
| Fine ceramic, P and DP | Blends and brightens with light cutting | Final edge and surface condition | Slower, less stock removal |
| Plastic, V to Z1 | Gentle cutting on soft alloys | Aluminum and thin-wall parts | Faster wear, less radius control |
| Steel balls and pins | Burnishes by plastic flow, not cutting | Brightening before coating | Cannot remove a burr, can fold one over |
| Porcelain and zirconia | Fine polish with negligible cutting | Small precision features | No deburring capability |
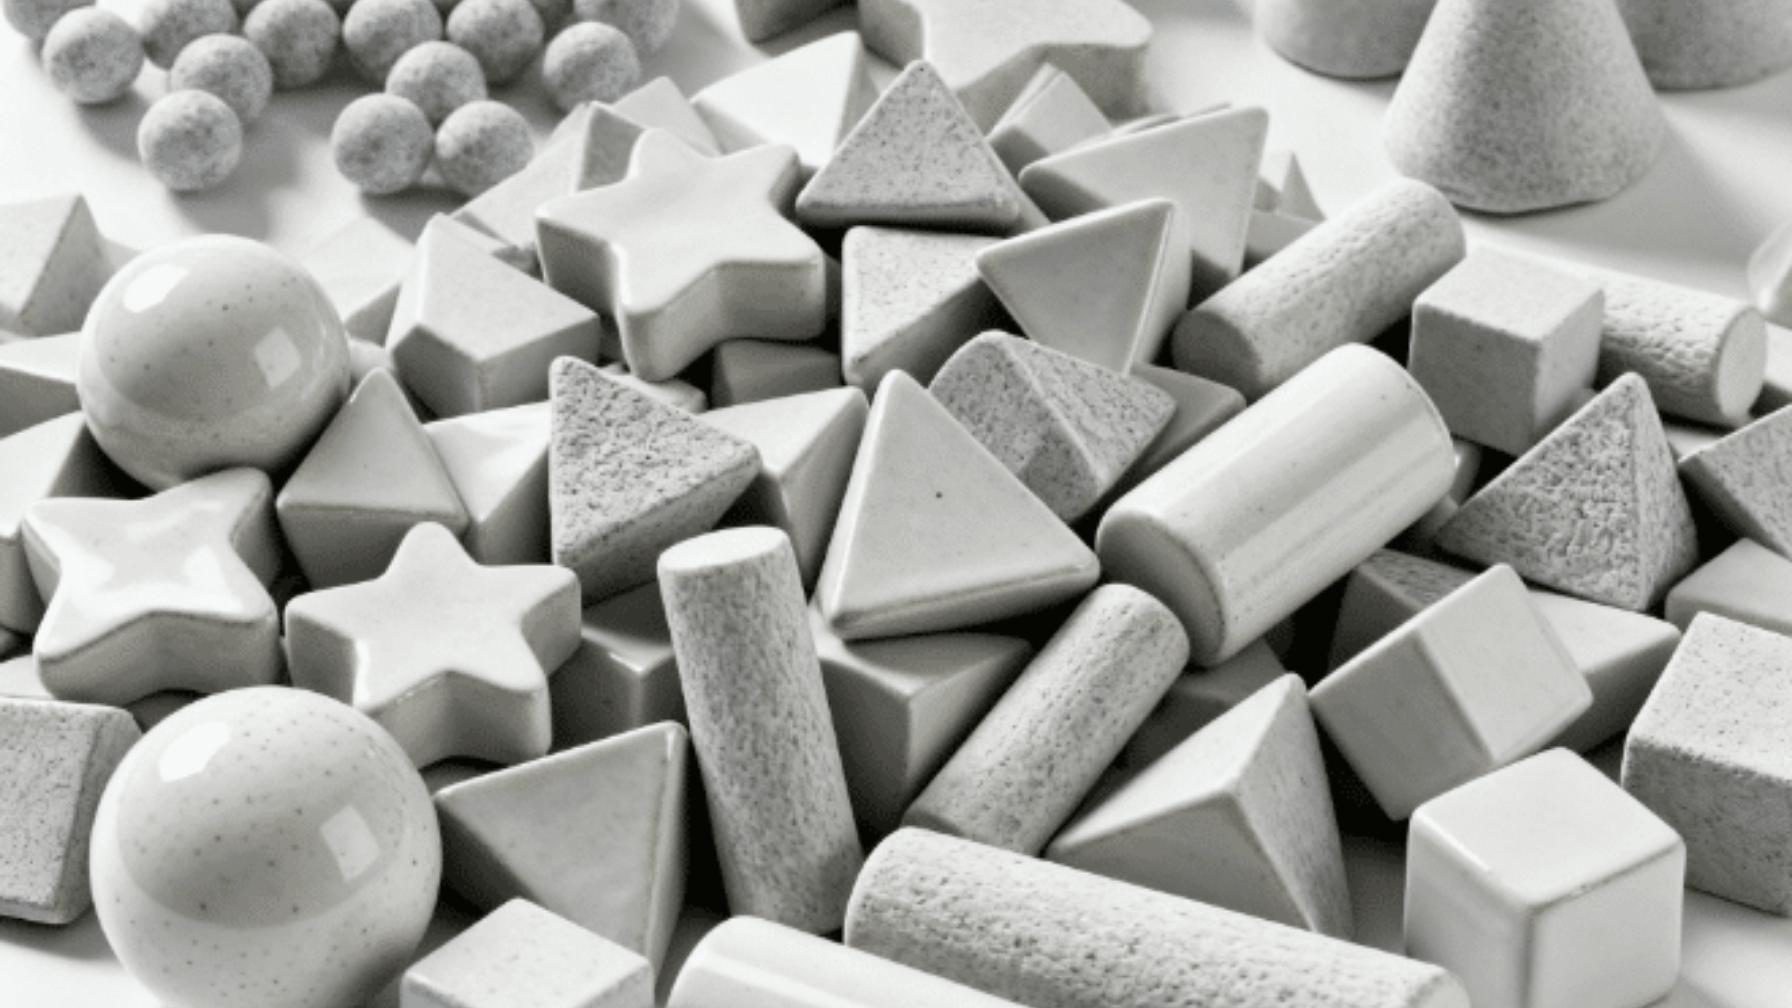
Shape matters as much as size. Triangular and tri-star shapes present a point to the edge and cut faster; cylinders and balls roll along the edge and blend more evenly. Media also has to enter and leave every feature it touches. If media can enter a slot but cannot turn inside it, it will lodge, and the part will be rejected at inspection for a reason that has nothing to do with the edge.
Media condition is a process variable, not a consumable detail. As ceramic media wears it becomes smaller and lighter, the cut rate falls, and the radius produced by a fixed cycle time drifts. A charge that produced an in-window radius when new will not do so after several hundred hours. That is why the control plan needs a media top-up rule and a screen for undersize media, and why a recipe copied from another shop rarely transfers without adjustment.
Compound carries the removed material away and keeps the media cutting instead of loading. Too little compound lets fines pack onto the media and smear the part, and the wrong pH can attack the alloy or leave a residue that interferes with the next operation. On aluminum, a compound that is not matched to the alloy can leave a dark surface that has to be removed before coating.
Titanium deserves separate handling. It galls, it work-hardens, and it is sensitive to contamination picked up from other alloys, which is why many shops keep a dedicated media charge and a dedicated compound for titanium work rather than sharing a bowl with steel parts. Where a bright finish is required after the edge is set, a fine paste matched to the alloy does the last step; AM 99, for instance, is formulated for titanium alloys.
A Process Development Sequence You Can Audit
A finishing recipe that works on one lot and not the next usually skipped a stage. The sequence below is written so that each step produces a record someone else can check.
- Fix the requirement in writing. Record the radius value and tolerance, the measurement method, the excluded surfaces and the acceptance authority. Required.
- Build a coupon that matches the worst feature. Same alloy, same machining operation, same cross-hole or thin wall. A flat test bar will not predict what happens at an intersection. Required.
- Record the incoming condition. Burr height under magnification, edge appearance, surface roughness where the drawing calls it, and the coolant or oil present on the parts. Without this baseline the trial cannot show what changed. Required.
- Stabilize the chemistry before changing the geometry. Run the first trials with one compound and one concentration, and vary media and time instead. Changing compound and media together produces a result nobody can reproduce. Required.
- Run a matrix, not a single point. Three media sizes or aggressiveness levels against three cycle times gives nine data points and a direction of change. One run gives a result with no trend behind it. Required.
- Measure with the agreed method, on several edges. One measurement on one edge of one part is not a capability study. Required.
- Write the control plan while the trial is still fresh. Cycle time, media charge and top-up, compound dose, screening interval, and the check that triggers requalification. Required.
- Add a fixture-based pass only where the loose process cannot hold the window. Optional, and usually the last cost to add.
A coupon run proves that this alloy, this feature, this media charge and this cycle produced that measured result. It does not prove the same setting holds when the media is worn, when the alloy lot changes, when the feature sits on a different face of the part, or when the machine is loaded to a different part-to-media ratio. Those are separate conditions and each needs its own check.
A trial result is only as useful as the conditions recorded around it. <Key to the Success of Finishing Process> covers the process factors that decide whether a finishing result repeats in production.
Keep the qualifying coupon as a physical reference and photograph the edges at magnification. When a question comes back six months later, a measurement number without a retained sample is difficult to defend.
Why Edge Quality Drifts and Where to Look First
Drift is normal. Media wears, compound concentration moves as water evaporates and drag-out removes chemistry, and the parts going in are never identical to the parts that set the recipe. What separates a controlled process from an uncontrolled one is whether the drift is detected before the parts ship.
| Symptom | Likely cause | First check |
|---|---|---|
| Radius grows over a production run | Media worn small, charge low | Screen the charge and compare media size with the qualifying sample |
| Corners over-broken at random | Part-on-part contact, parts jamming | Check load ratio and how parts move in the bowl |
| Burr remains in a cross-hole | Media cannot enter the intersection | Compare media size with the hole diameter, test a smaller shape |
| Edge measures out of tolerance but looks polished | Metal folded over rather than cut | Review media type and compound dose for that step |
| Staining after a wet process | Compound residue or slow drying | Check concentration, rinse quality and dry time |
Treat the middle column as a hypothesis until the check confirms it. Changing three variables at once will usually make the symptom disappear for a shift and return without an explanation, which is worse than the original problem because the process is now undocumented.
Where a check cannot decide between two causes, isolate one variable on a small batch rather than on the production order. A twenty-piece run that settles the question costs less than a rejected lot.
What to Record and What to Send With Your Samples
Drawings alone rarely settle the question of whether a process will hold the edge. The information below is what a finishing evaluation actually needs, and most of it comes from documents the shop already has.
| Field | What to send | Why it matters |
|---|---|---|
| Alloy and temper | Material specification and heat treat condition | Sets media and compound compatibility and the cut rate |
| Edge callout | The exact note with value and tolerance | “Break sharp edges” cannot be measured or accepted |
| Measurement method | The instrument or gauge the customer accepts | A process proven on a different instrument is not proven |
| Excluded surfaces | Threads, seal faces, bearing seats, datum edges | Prevents a correct edge from damaging a functional surface |
| Incoming condition | Machining method, burr size, coolant residue | Explains the burr the process has to remove |
| Volume and part size | Monthly quantity, largest and smallest dimensions | Drives machine choice and loading |
Send parts that represent the worst case: the smallest cross-hole, the thinnest wall, the edge closest to a sealing face. A sample of convenient parts will produce a convenient result that does not survive the first difficult order.
Send Sample Parts and Get a Measured Edge Result
The fastest way to settle whether a mass finishing process can hold your edge callout is to run your own parts. Send five to twenty pieces that include the worst feature on the drawing, with the alloy and temper, the edge callout and its tolerance, the measurement method your customer accepts, the surfaces that must not be touched, the burr condition coming off the machine, and the monthly volume. Mass Polishing will run them on the matching machine and media combination and report the measured edge radius and surface condition, so the decision rests on a result rather than an estimate. Dennis and the process team handle sample evaluation, and you can reach them through the contact form at masspolishing.com.
FAQ
Can mass finishing replace hand deburring on aerospace parts?
Often, but not always. A loose-media process handles the general edge work on most machined parts and does it more consistently than a bench operator working through a batch. It stops being enough when the burr sits where media cannot reach, when the drawing calls a radius with a tolerance the process cannot hold across the batch, or when one over-broken corner would scrap a high-value part. In those cases the machine still removes the bulk of the burr and a controlled secondary operation finishes the edge.
What edge radius can a vibratory or centrifugal process hold?
There is no universal number, and a supplier who quotes one without seeing the part is guessing. The radius depends on media size and condition, the alloy, the cycle time, and how well the feature is exposed to media flow. A trial on your own parts, measured with the instrument your customer uses, is the only reliable answer. The direction of change is predictable: finer media and shorter cycles give a smaller radius, coarser media and longer cycles give a larger one.
How do you stop media lodging in cross-holes and slots?
Match media size to the smallest feature, and check the shape as well as the size. Media enters a feature far more easily than it leaves, so a slot that accepts a triangular piece at an angle may hold it. Screening the charge, choosing a shape that cannot wedge, and inspecting the smallest features before packing prevent most of it. Where a feature is unavoidable, a fixture-based process that keeps media moving in one direction is easier to control than a loose bowl.
Does titanium need its own media and compound?
Many shops run it that way. Titanium work-hardens, galls, and is sensitive to contamination picked up from other alloys, so a shared charge with steel parts introduces risk that is hard to see on the finished surface. A dedicated media charge, a compound matched to the alloy, and a separate finishing sequence remove that risk. Where a bright final finish is needed, a paste formulated for titanium completes the edge work without changing the radius.
If you’re interested, check out these related articles:
Troubleshooting of Centrifugal Drum Finishing Machines
How to Extend the Service Life of Automatic Polishing Machine