
Oxide removal from hardware is the step that determines whether a later finish holds or fails. Plating and coating lines cannot hide heat scale, rust, or zinc corrosion, because these residues leave voids, weak adhesion, and cloudy deposits. We treat oxide removal as a preparation problem for the alloy, oxide thickness, and final surface, not as a single chemical dip. This article explains how to set up that pre finishing stage so brass, steel, and zinc hardware reaches the polishing or plating line with clean, uniform, active metal.
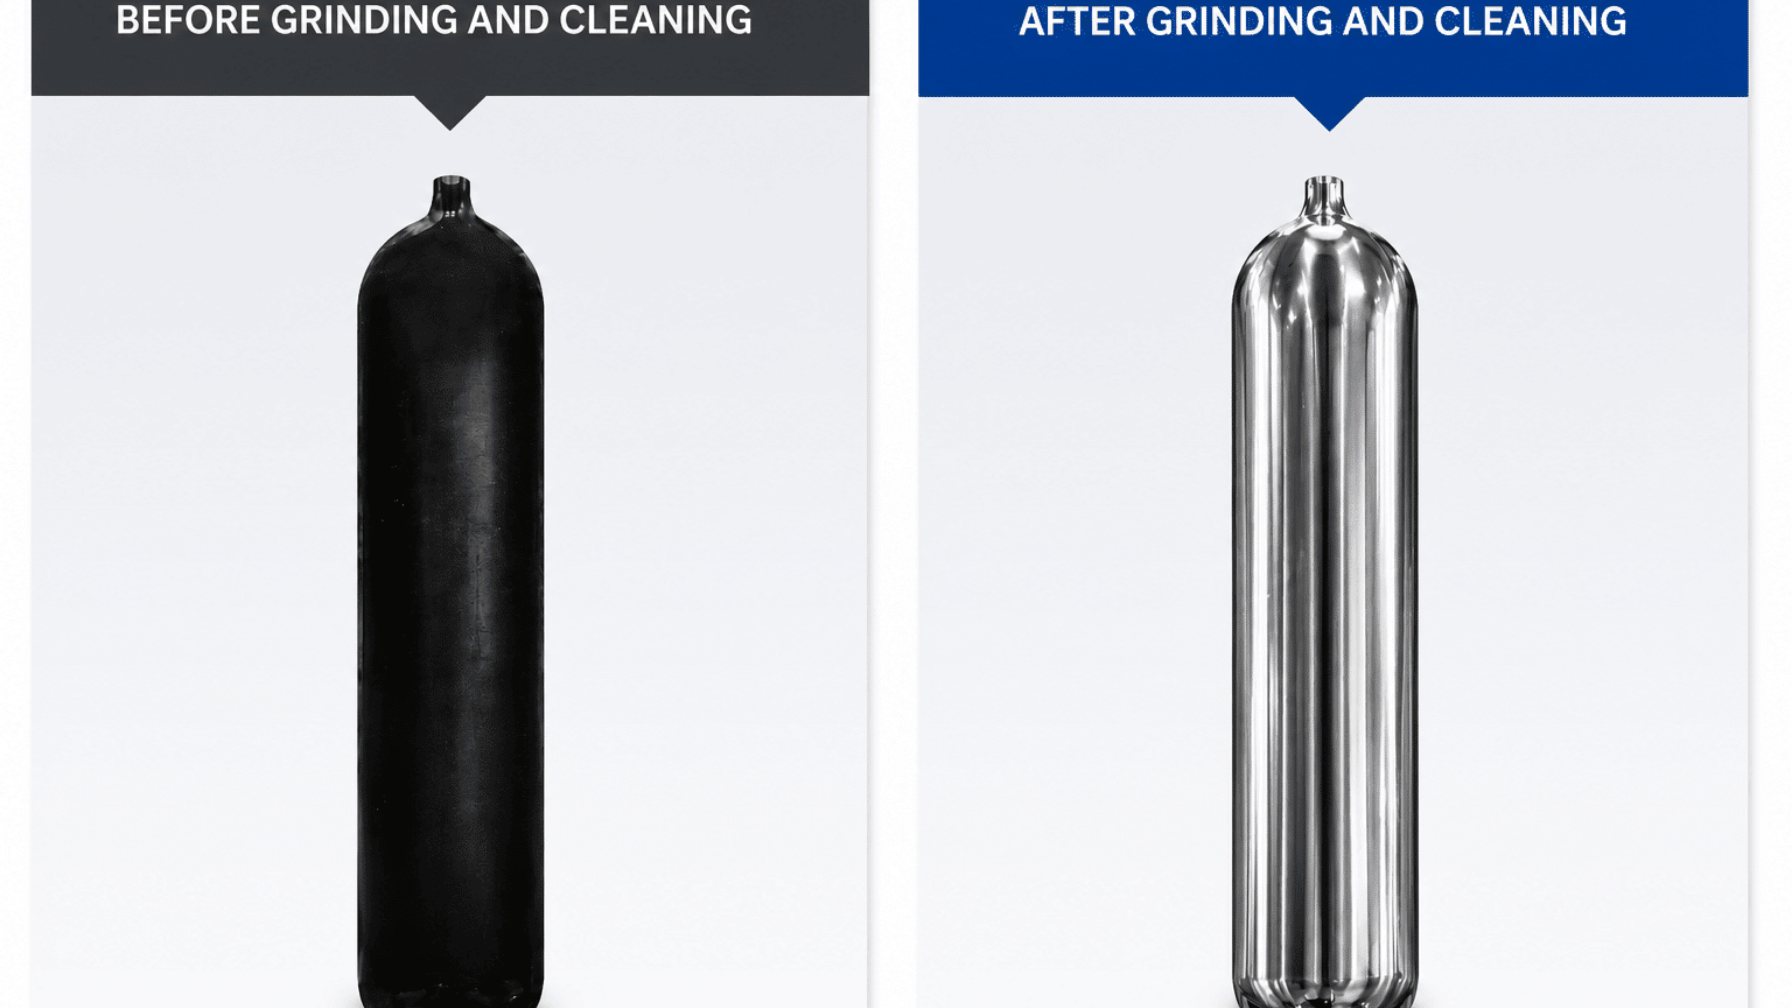
What Does Oxide Removal from Hardware Actually Need to Achieve?
Oxide removal from hardware has two jobs: strip the outer scale or corrosion layer and leave the base metal smooth enough for the next process. A bright surface is not the same as a clean surface. Heat scale from forging or annealing is hard, brittle, and chemically different from the base metal. Rust on carbon steel is porous and traps oil. Tarnish on brass is a thin copper and zinc oxide film that can pass into a plating bath if not removed. White corrosion on zinc die castings is not simply surface dust; it is an adherent zinc hydroxide and zinc carbonate layer that blisters under plated deposits.
That is why we check three results before a part leaves pre finishing. First, no visible oxide remains in threads, blind holes, or lettering. Second, the surface is uniform to the eye, without bright patches alternating with dull oxide. Third, the part does not flash rust or tarnish again within the time it waits for plating.
| Hardware material | Typical oxide or scale | Preferred removal route | Pre finishing watch point |
|---|---|---|---|
| Carbon steel | Mill scale, red rust | Acid pickling or aggressive ceramic media, then alkaline rinse | Flash rust before plating |
| нержавеющая сталь | Heat tint, weld oxide | Acid cleaning or ceramic finishing | Over etching at grain boundaries |
| Brass and bronze | Tarnish, cuprous oxide | Mild acid bright dip or fine plastic media | Copper redeposition in rinses |
| Zinc die cast | White corrosion, zinc oxide | Mild alkaline or plastic media, avoid strong acid | Surface pitting under plated layer |
| Plated hardware | Corrosion through damaged coating | Strip or spot clean, then re plate | Base metal attack behind coating |
Which Oxide Removal Process Works for Brass, Steel, and Zinc Hardware?
Hardware is rarely one alloy, so a single pickling bath is usually the wrong starting point. We separate oxide removal methods by how aggressive the oxide is and how soft the substrate is.
Brass and Bronze Hardware
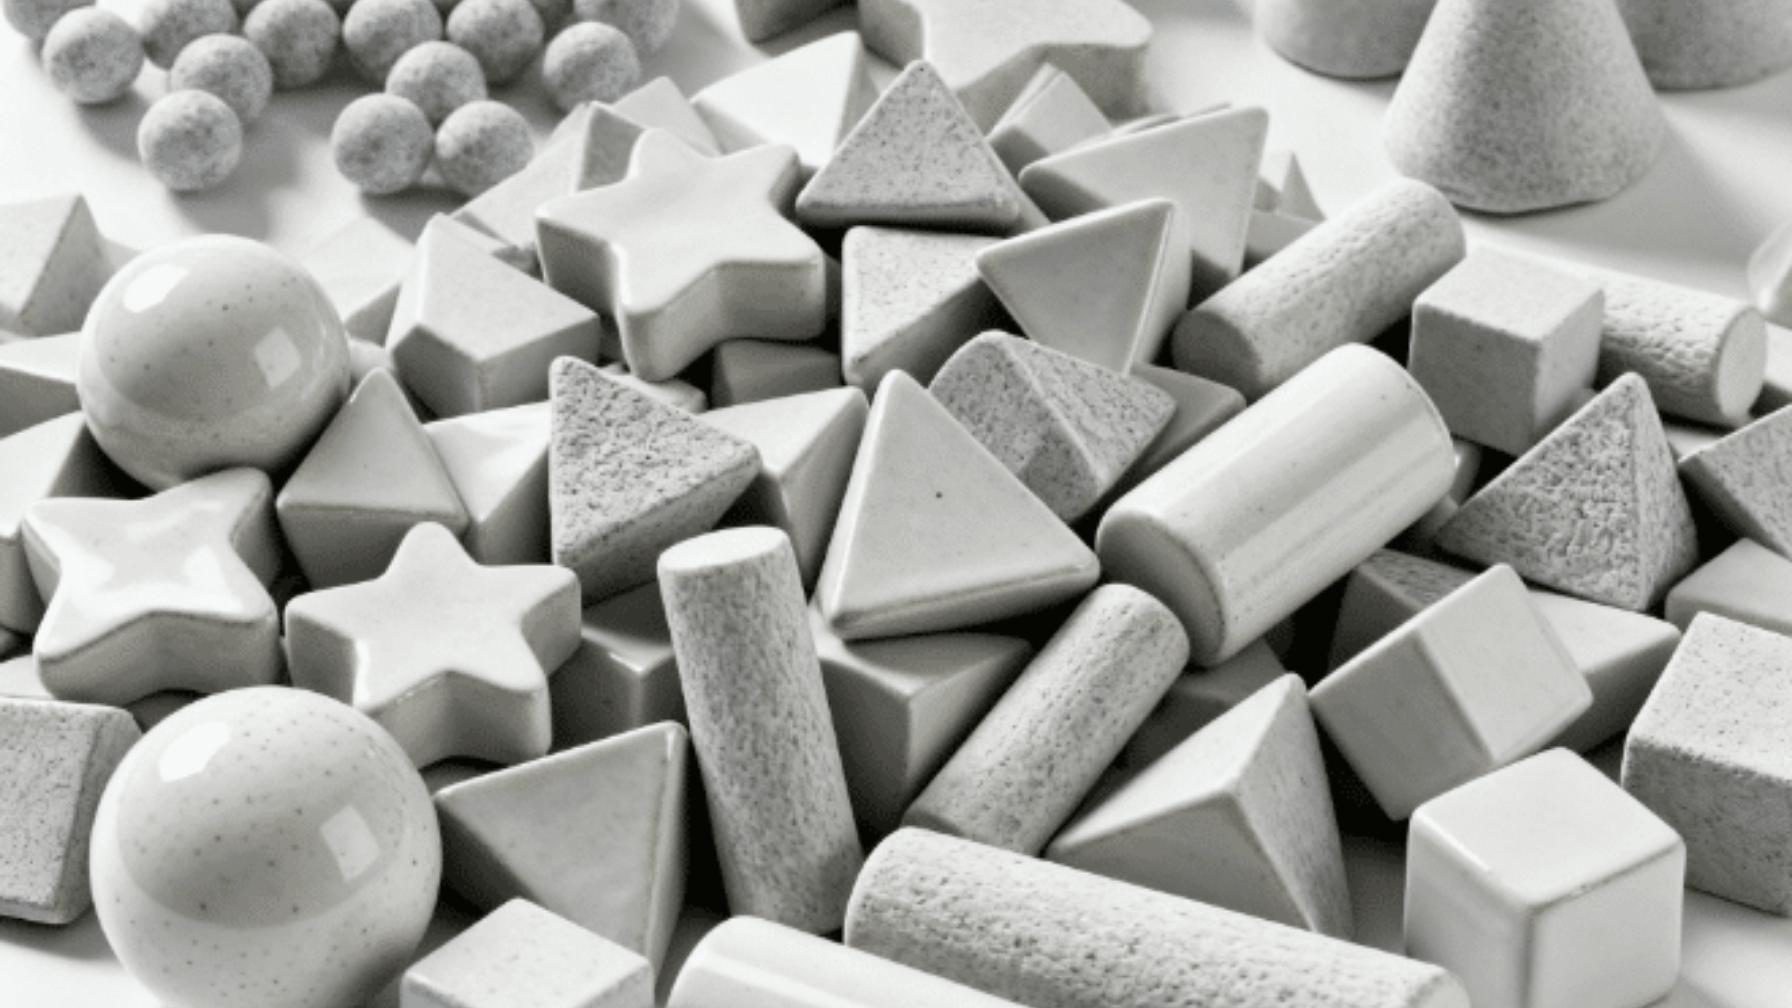
Brass tarnish and fire scale respond to a short mild acid dip or an acidic cleaning compound. For mechanical work, plastic media in a vibratory bowl removes the oxide film without cutting deep into the soft metal. We use a fine pre plate plastic media such as the V grade because the 1500 grit abrasive leaves the smooth, bright surface that electroplating needs. If the parts carry deeper oxide from casting or brazing, a light ceramic cut followed by a higher shine step works better than one aggressive step.
Carbon Steel and Stainless Steel Hardware
Carbon steel mill scale and red rust require stronger mechanical or chemical action. Ceramic media in the FC, TC, or SC ranges gives the cutting work needed to break scale from threads and corners. For stainless steel heat tint, the mechanical route may not reach deep into narrow recesses; an acid cleaning step is often required first. The point is to remove the oxide, not to smear it into the surface. A smeared surface looks uniform but fails adhesion testing later.
Zinc Die Cast and Plated Hardware
Zinc die castings need a gentler path. Strong acid can open porosity and create pits that only appear after plating. A mild alkaline cleaner or a plastic deburring media removes white corrosion without attacking the zinc surface. The process then moves to a fine pre plate media before the parts go into the plating bath. The same principle applies to hardware that is already plated but shows corrosion through damaged coating: strip only the affected area when possible, then re clean and re plate.
Zinc die cast hardware is sensitive to both acid attack and surface smearing, so the oxide removal step should be treated as part of plating preparation rather than as a separate heavy cut. <Polishing Zinc Die Castings in Vibratory Tumbling Machines a Comprehensive GuidecURL Too many subrequests by single Worker invocation. To configure this limit, refer to https://developers.cloudflare.com/workers/wrangler/configuration/#limits.
cURL Too many subrequests by single Worker invocation. To configure this limit, refer to https://developers.cloudflare.com/workers/wrangler/configuration/#limits Вибрационная отделка cURL Too many subrequests by single Worker invocation. To configure this limit, refer to https://developers.cloudflare.com/workers/wrangler/configuration/#limits
cURL Too many subrequests by single Worker invocation. To configure this limit, refer to https://developers.cloudflare.com/workers/wrangler/configuration/#limits.
cURL Too many subrequests by single Worker invocation. To configure this limit, refer to https://developers.cloudflare.com/workers/wrangler/configuration/#limits.
cURL Too many subrequests by single Worker invocation. To configure this limit, refer to https://developers.cloudflare.com/workers/wrangler/configuration/#limits.
cURL Too many subrequests by single Worker invocation. To configure this limit, refer to https://developers.cloudflare.com/workers/wrangler/configuration/#limits.
cURL Too many subrequests by single Worker invocation. To configure this limit, refer to https://developers.cloudflare.com/workers/wrangler/configuration/#limitscURL Too many subrequests by single Worker invocation. To configure this limit, refer to https://developers.cloudflare.com/workers/wrangler/configuration/#limitscURL Too many subrequests by single Worker invocation. To configure this limit, refer to https://developers.cloudflare.com/workers/wrangler/configuration/#limits.
cURL Too many subrequests by single Worker invocation. To configure this limit, refer to https://developers.cloudflare.com/workers/wrangler/configuration/#limits.
cURL Too many subrequests by single Worker invocation. To configure this limit, refer to https://developers.cloudflare.com/workers/wrangler/configuration/#limits
cURL Too many subrequests by single Worker invocation. To configure this limit, refer to https://developers.cloudflare.com/workers/wrangler/configuration/#limits.
-
cURL Too many subrequests by single Worker invocation. To configure this limit, refer to https://developers.cloudflare.com/workers/wrangler/configuration/#limits.
-
cURL Too many subrequests by single Worker invocation. To configure this limit, refer to https://developers.cloudflare.com/workers/wrangler/configuration/#limits.
-
cURL Too many subrequests by single Worker invocation. To configure this limit, refer to https://developers.cloudflare.com/workers/wrangler/configuration/#limits.
-
cURL Too many subrequests by single Worker invocation. To configure this limit, refer to https://developers.cloudflare.com/workers/wrangler/configuration/#limits.
cURL Too many subrequests by single Worker invocation. To configure this limit, refer to https://developers.cloudflare.com/workers/wrangler/configuration/#limits
cURL Too many subrequests by single Worker invocation. To configure this limit, refer to https://developers.cloudflare.com/workers/wrangler/configuration/#limits.
cURL Too many subrequests by single Worker invocation. To configure this limit, refer to https://developers.cloudflare.com/workers/wrangler/configuration/#limitsАвтоматическая очистка сточных вод. Устойчивое водооборотное производство для массовой обработкиcURL Too many subrequests by single Worker invocation. To configure this limit, refer to https://developers.cloudflare.com/workers/wrangler/configuration/#limits.
cURL Too many subrequests by single Worker invocation. To configure this limit, refer to https://developers.cloudflare.com/workers/wrangler/configuration/#limits.
cURL Too many subrequests by single Worker invocation. To configure this limit, refer to https://developers.cloudflare.com/workers/wrangler/configuration/#limits
cURL Too many subrequests by single Worker invocation. To configure this limit, refer to https://developers.cloudflare.com/workers/wrangler/configuration/#limits
cURL Too many subrequests by single Worker invocation. To configure this limit, refer to https://developers.cloudflare.com/workers/wrangler/configuration/#limits.
cURL Too many subrequests by single Worker invocation. To configure this limit, refer to https://developers.cloudflare.com/workers/wrangler/configuration/#limits
cURL Too many subrequests by single Worker invocation. To configure this limit, refer to https://developers.cloudflare.com/workers/wrangler/configuration/#limits.
cURL Too many subrequests by single Worker invocation. To configure this limit, refer to https://developers.cloudflare.com/workers/wrangler/configuration/#limits
cURL Too many subrequests by single Worker invocation. To configure this limit, refer to https://developers.cloudflare.com/workers/wrangler/configuration/#limits.
cURL Too many subrequests by single Worker invocation. To configure this limit, refer to https://developers.cloudflare.com/workers/wrangler/configuration/#limits
cURL Too many subrequests by single Worker invocation. To configure this limit, refer to https://developers.cloudflare.com/workers/wrangler/configuration/#limits cURL Too many subrequests by single Worker invocation. To configure this limit, refer to https://developers.cloudflare.com/workers/wrangler/configuration/#limits cURL Too many subrequests by single Worker invocation. To configure this limit, refer to https://developers.cloudflare.com/workers/wrangler/configuration/#limits.
Если вас интересует, ознакомьтесь с этими связанными статьями:
cURL Too many subrequests by single Worker invocation. To configure this limit, refer to https://developers.cloudflare.com/workers/wrangler/configuration/#limits
Stainless Steel Walnut Zirconic Finishing Media