
Bracelet chain and link polishing rarely fails because the abrasive is too weak. It fails because chain links tangle, clasps strike each other, and media wedge inside hollow links, leaving the piece bright in some areas and dull in others. A batch process built around the right machine, media shape, and load ratio removes that variability. We recommend a two-stage route for most bracelet work: vibratory finishing for rapid edge softening and scale removal, followed by dry barrel or centrifugal disc polishing for the final mirror or satin surface. The choice is less about machine brand than about keeping flexible links moving separately against the media.
Batch Finishing Logic for Bracelet Chain and Link Work
Most bracelet finishing problems come from treating a flexible assembly like a solid casting. A solid part can be pressed, tumbled, and inspected as one shape. A chain bracelet is a series of moving joints; when the load rotates, those joints open and close, pinch media, and transmit impact into the clasp and the softer soldered points. The process must therefore protect link edges without isolating the surfaces that need contact with abrasive.
Dense loading usually makes the finish worse because it restricts the rolling action between links. Our team has found that a lower fill level with shaped ceramic or plastic media produces a more even cut than a full bowl with cheaper random media. The objective is not brightness alone, but consistent contact across every visible surface while the chain moves as a loose cloud of parts.
Tumbler – Jewelry Polishing)
Machine Choices for Chain and Link Polishing
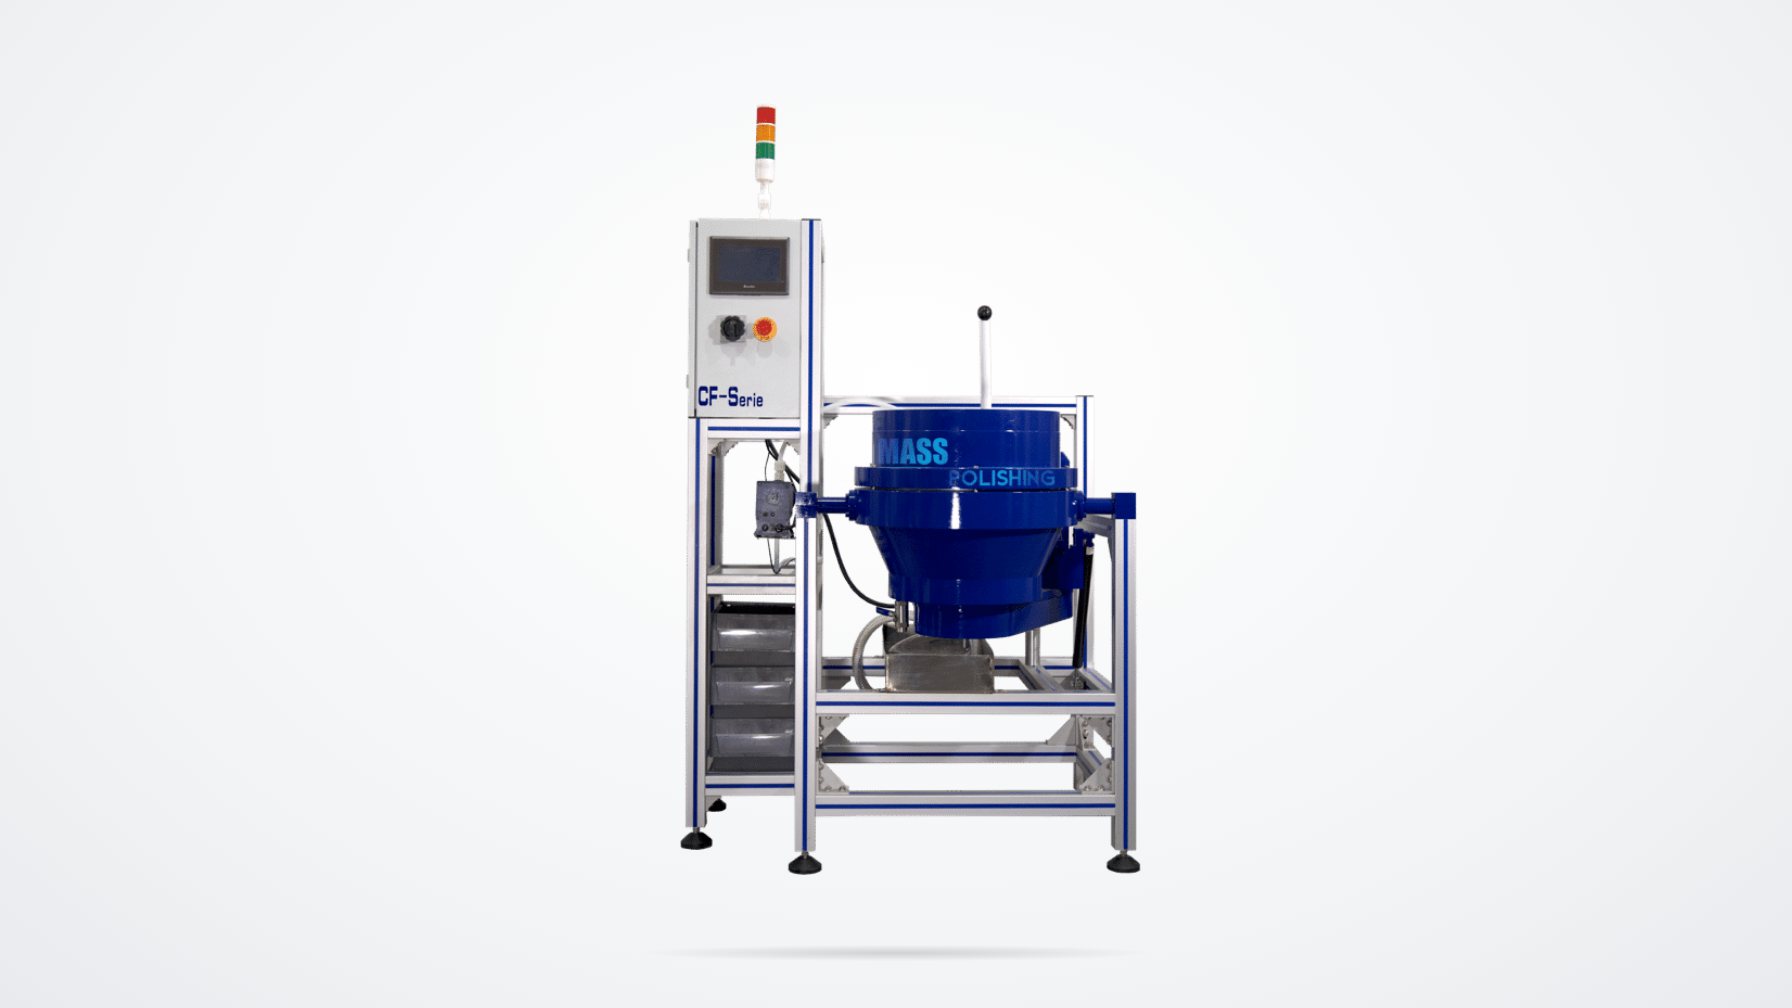
Machine selection changes what the process can accomplish before an operator touches the parts. For first-stage cutting on assembled bracelets, the SW series vibratory bowl is our default because the motion is gentle enough to keep links separated while still radiusing sharp edges left by stamping and casting. EB series centrifugal barrel machines move faster and suit workpieces that have already passed a first cut or that need a bright finish on solid bangles. ED, PD, and CF centrifugal disc machines provide better gap control and are well matched to fine link work where media must reach inner surfaces without hammering the metal.
MF series magnetic pin systems are finishing aids, not a replacement for bulk surface work. They reach hollow link interiors and clasp recesses but move far less material than a true barrel or disc process.
| Tipo de máquina | Best bracelet task | Chain and link consideration |
|---|---|---|
| Cuba vibratoria | Deburring, radiusing, first-stage satin work | Low force keeps long chain moving with less tangling |
| Cilindro centrífugo | Fast edge rounding and bright finishing | High energy requires smaller media and controlled load |
| Disco centrífugo | Precision work on fine links | Gap control protects thin sections and soldered points |
| Magnetic pin | Inner corners and clasp recesses | Reaches hollows but does not replace bulk finishing |
Vibratory finishing is often the lowest-cost way to handle the first cut on flexible chain. <Why Buy a Vibratory Tumbler> explains the load and motion trade-offs that matter when the goal is to keep long linked parts moving without the nesting problems common in more aggressive barrel systems.
Media and Compound Pairing for Uniform Bracelet Surface Finishing
Media shape does more work in bracelet finishing than media color or grit. For open link chains, we specify shapes that cannot wedge easily: small angle-cut cylinders, cones, or spherical ceramic and porcelain media. Round media rolls across outer link surfaces and leaves sharp internal edges unfinished. A mixed shape load works better because smaller shapes enter the link gaps while larger shapes carry the surface cut.
For gold-filled, silver, or plated brass bracelets, we pair ceramic pre-polish media with a mild alkaline compound to remove oxide and light scratches without etching the base metal. For final mirror work on stainless steel or precious metal, dry polishing with fine porcelain granules or walnut shell produces high gloss without the water spotting risk of a wet final pass.
Machine – Dry Barrel Finishing)
Selecting media by shape is more important than selecting by material in chain work. <Tumbling Media Selection> covers how angle-cut shapes, pin shapes, and spheres penetrate differently, which directly affects whether hollow link interiors receive any finishing at all.
If your bracelets mix hollow links with gemstone settings, plating, or soldered findings, confirm media size and compound pH before locking the bill of materials. A fast test on sample links avoids the expensive discovery that a finishing step was cutting in the wrong place. Send your part drawings and sample links to [email protected], and we will recommend a starting recipe.
Handling Risks and Building a Repeatable Bracelet Finishing Process
Risk control is where chain finishing separates experienced shops from beginners. Tangling happens when long chain segments wrap around themselves; this can be reduced with lower bowl speed, shorter chain lengths in the batch, and a divider or fixture for high-value pieces. Clasp damage occurs because the clasp is the heaviest part of the assembly and receives the most impact. We inspect clasp tongues and jump rings after every test run before committing to production.
Media lodging is the most overlooked failure. Fine particles enter hollow links during wet cutting and stay there until the final cleaning stage. Anti-adhesion beads and a properly adjusted separation screen reduce that problem without leaving residue.
- Sort workpieces by alloy, plating condition, and link size.
- Fill the bowl or barrel to 60 to 70 percent volume with the selected media and compound, then add a reduced part load.
- Run a short first cycle and inspect link interiors, not just outer surfaces.
- Move to dry fine polishing only after the cut is uniform; skip dry finishing if water remains in hollow links.
- Separate, rinse, and dry completely before final plating, assembly, or packaging.
Machine – Magnetic Polishing)
If the target is a bright shine on stainless steel bracelets, the final burnishing step changes the outcome. <Pulido de bolas de acero inoxidable explorando sus efectos en las propiedades superficiales> explains how ball media contributes to gloss after the cutting stage, which is useful after a dry polish has leveled the surface.
cURL Too many subrequests by single Worker invocation. To configure this limit, refer to https://developers.cloudflare.com/workers/wrangler/configuration/#limits
cURL Too many subrequests by single Worker invocation. To configure this limit, refer to https://developers.cloudflare.com/workers/wrangler/configuration/#limits.
cURL Too many subrequests by single Worker invocation. To configure this limit, refer to https://developers.cloudflare.com/workers/wrangler/configuration/#limits
cURL Too many subrequests by single Worker invocation. To configure this limit, refer to https://developers.cloudflare.com/workers/wrangler/configuration/#limits
cURL Too many subrequests by single Worker invocation. To configure this limit, refer to https://developers.cloudflare.com/workers/wrangler/configuration/#limits.
cURL Too many subrequests by single Worker invocation. To configure this limit, refer to https://developers.cloudflare.com/workers/wrangler/configuration/#limits
cURL Too many subrequests by single Worker invocation. To configure this limit, refer to https://developers.cloudflare.com/workers/wrangler/configuration/#limits.
cURL Too many subrequests by single Worker invocation. To configure this limit, refer to https://developers.cloudflare.com/workers/wrangler/configuration/#limits
cURL Too many subrequests by single Worker invocation. To configure this limit, refer to https://developers.cloudflare.com/workers/wrangler/configuration/#limits.
cURL Too many subrequests by single Worker invocation. To configure this limit, refer to https://developers.cloudflare.com/workers/wrangler/configuration/#limits
cURL Too many subrequests by single Worker invocation. To configure this limit, refer to https://developers.cloudflare.com/workers/wrangler/configuration/#limits.
Si está interesado, consulte estos artículos relacionados:
Cómo reducir la contaminación acústica de la máquina de pulido automática
cURL Too many subrequests by single Worker invocation. To configure this limit, refer to https://developers.cloudflare.com/workers/wrangler/configuration/#limits