
Steel machining deburring for milled and turned parts fails most often when one process is expected to remove every burr the same way. A heavy rolled-over burr at a drilled intersection needs more energy than a fine feather edge on a turned shoulder, and tighter part dimensions leave less room for stock removal. At Mass Polishing, our position is direct: remove the burr with the least possible edge disturbance, then refine the surface only if the print calls for it. That sequence protects threads, sealing faces, and close-tolerance dimensions while leaving parts safe to handle, measure, and assemble.
Steel Machining Deburring and the Burr Types That Drive Process Choices
On a milled steel part, burr location usually tells you how it formed. Climb milling tends to leave a thin sharp edge on the exit side of the cut, while conventional milling can roll a heavier burr when the chip separates. Turning behaves the same way at shoulders and thread runouts. A light feed line may leave a fine radial burr, and an interrupted cut or worn insert can tear a thicker root. This matters because burr type, not part count, should set the first process decision. A thin foil edge often clears quickly with light-cut ceramic media in a vibratory bowl, but a rooted mill burr may need centrifugal barrel energy before the edge is safe.
In our sample reviews, I record material, hardness, burr root thickness or a magnified photo, and every dimension that cannot change. Those facts decide whether an SW series vibratory bowl, an EB centrifugal barrel machine, or a finition par dragage pass is the right starting point. Guessing at this stage creates scrap. An aggressive ceramic triangle can reach a buried burr quickly but also cut a thread crest or wash out a sharp edge if the cycle is not watched.
Machine – Deburring)
For machined steel parts with heavy edges or hardened material, high-energy processing often shortens the path to a uniform edge break. <Machines d'ébavurage par baril centrifuge Solutions de finition de masse à haute efficacité> covers how centrifugal barrel action removes rooted burrs faster than conventional vibratory processing on small hardened steel components.
Media and Machine Selection for Milled and Turned Steel Parts
Steel parts can tolerate most ceramic media shapes as long as the media size reaches the feature. Through holes, keyways, and narrow grooves require media small enough to enter without lodging. Very small media cut more slowly, so a part with both a wide external burr and a narrow internal burr may need a two-step process rather than one compromised media size. Ceramic TC, FC, and SFC grades handle hard steel edges, while P and DP grades refine the surface after cutting. Porcelain or stainless steel media are not the first choice for rooted burrs; they brighten a surface but remove less stock per hour.
| Finishing requirement | Type de machine | Typical media selection |
|---|---|---|
| Thin feather edges on carbon steel | SW or SWS vibratory bowl | Ceramic light cut or general cut |
| Rooted mill burrs on hardened steel | EB centrifugal barrel | Ceramic fast cut or super fast cut |
| Controlled edge radius on precision parts | DF drag finishing | Fine ceramic or polishing media |
| Long turned shafts or thin stems | TV vibrateur tubulaire | Ceramic general cut with dividers |
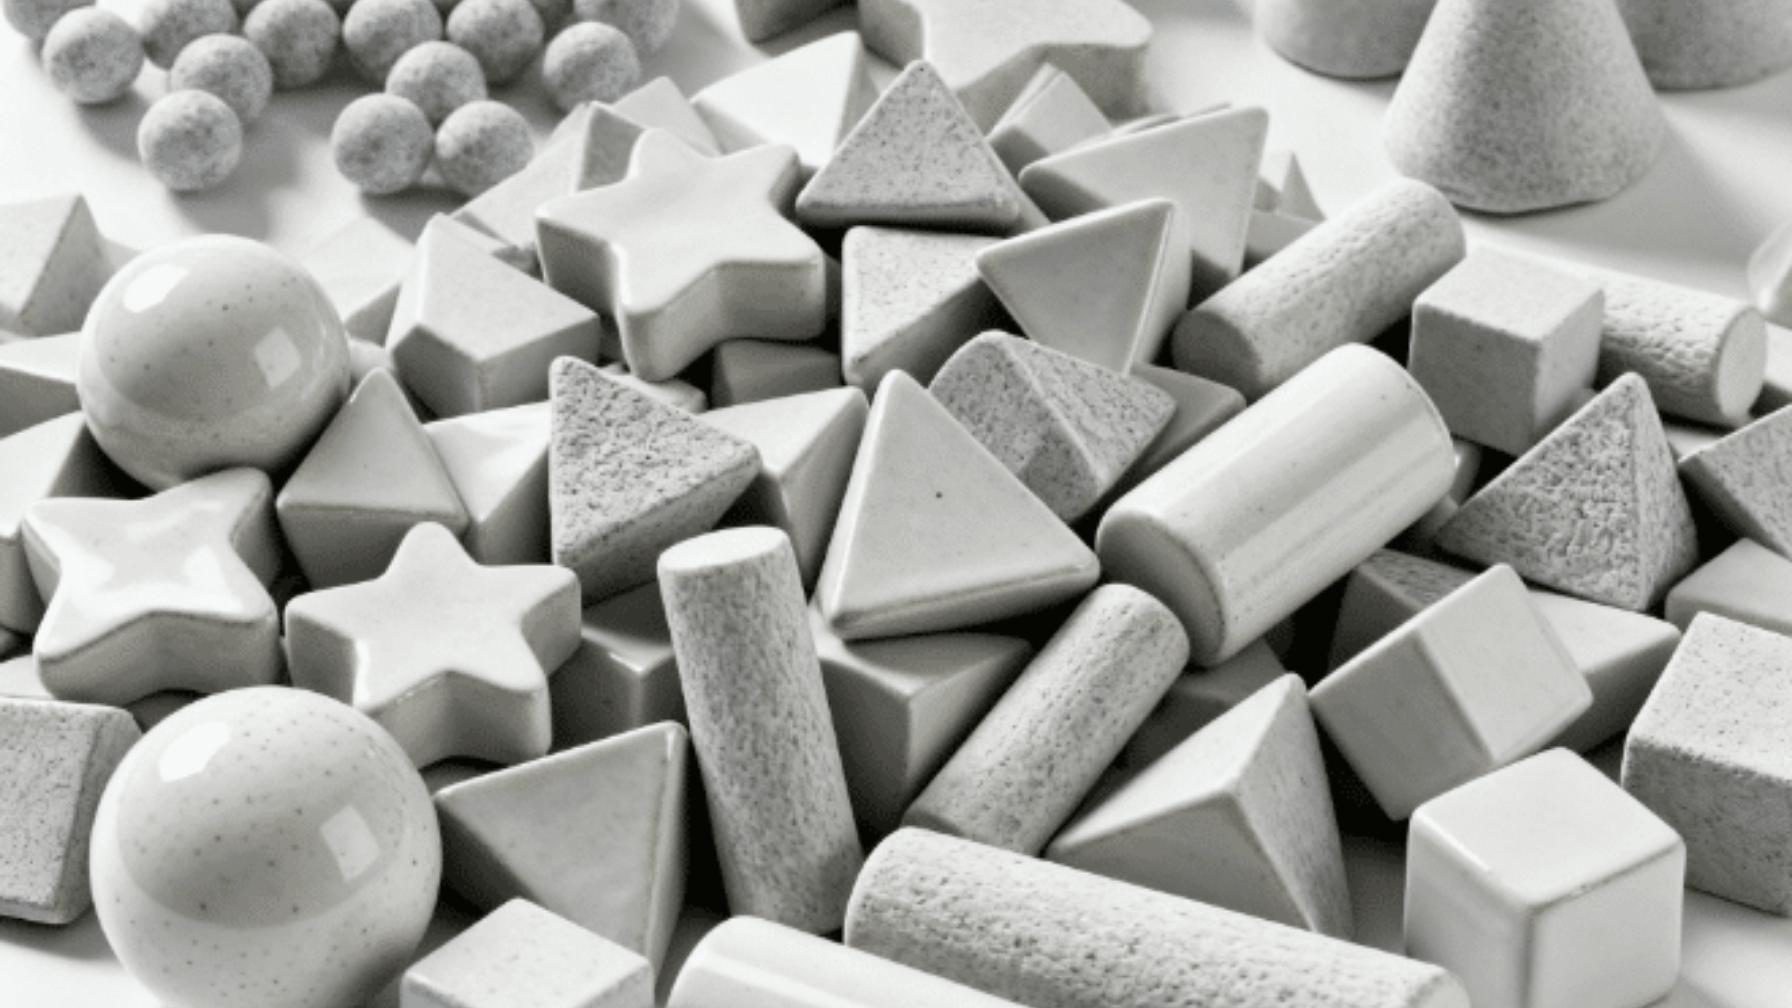
If the goal is gentler edge rounding on larger steel parts rather than fast burr removal, barrel tumbling is the lower-risk choice. <Le secret des finitions parfaites : le tumbling en baril rotatif> explains how rotary barrel wet processing produces even edge breaks on mixed machined parts without the impact intensity of a high-energy system.
Wet processing keeps steel fines suspended and reduces smearing. For carbon steel deburring, LC10 general purpose compound works as a cleaner and light deruster during the same cycle. If the parts are oily, LC13 degreasing compound is the better first stage. The compound is not a replacement for media selection; it changes how cleanly the cut runs.
Cycle Time and Surface Finish Trade-Offs in Steel Deburring
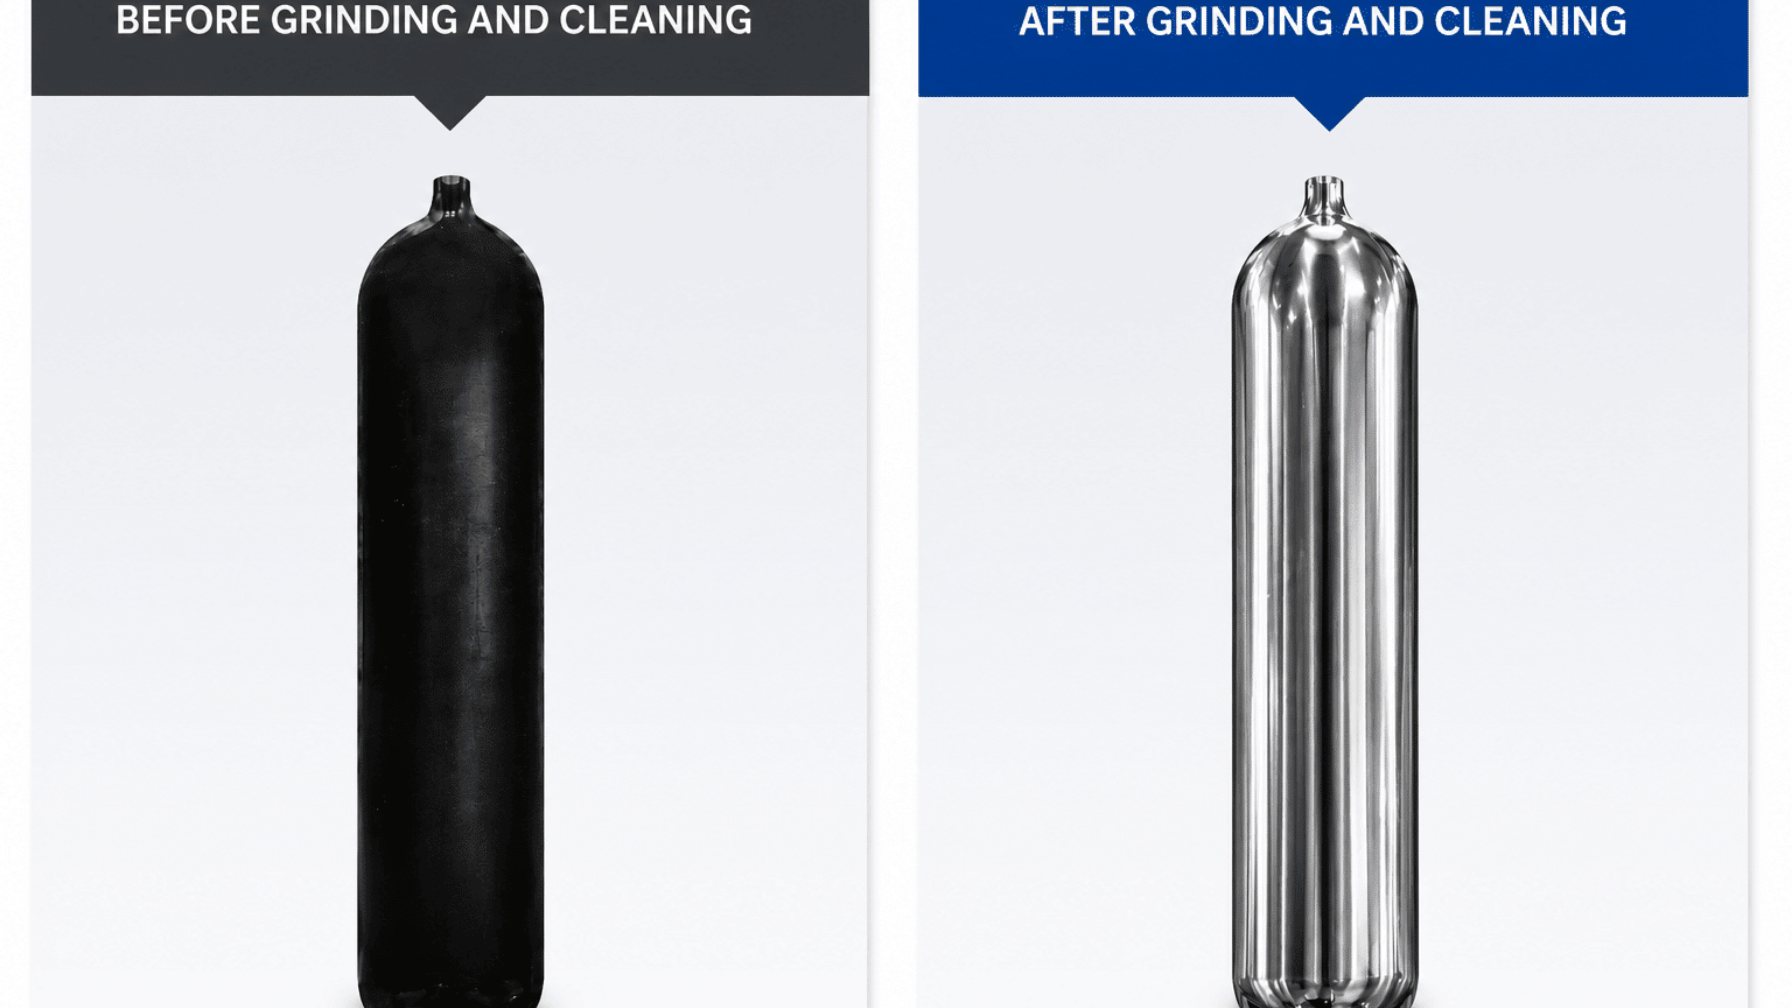
Deburring steel in a vibratory bowl is usually measured in 20 to 60 minute cycles, depending on burr root and media. Centrifugal barrel processing compresses the same work into a fraction of that time but applies far more energy to the edge. The trade-off is edge radius control. If a drawing permits a 0.1 mm edge break, a short high-energy pass can be the lowest-cost route. If the maximum radius is 0.05 mm or the part has a sharp sealing edge, I would keep the energy lower and accept a longer vibratory or drag finishing cycle. Surface finish follows the same logic. Aggressive cutting leaves a matte finish first, and brightness comes only after the burr is gone.
If your program involves an edge radius below 0.1 mm on a sealing face or bearing shoulder, confirm the media size and cycle time before committing the process. Send a drawing to [email protected] and we can shortlist which machine class will hold that edge.
Process Control for Thin-Wall and Close-Tolerance Steel Parts
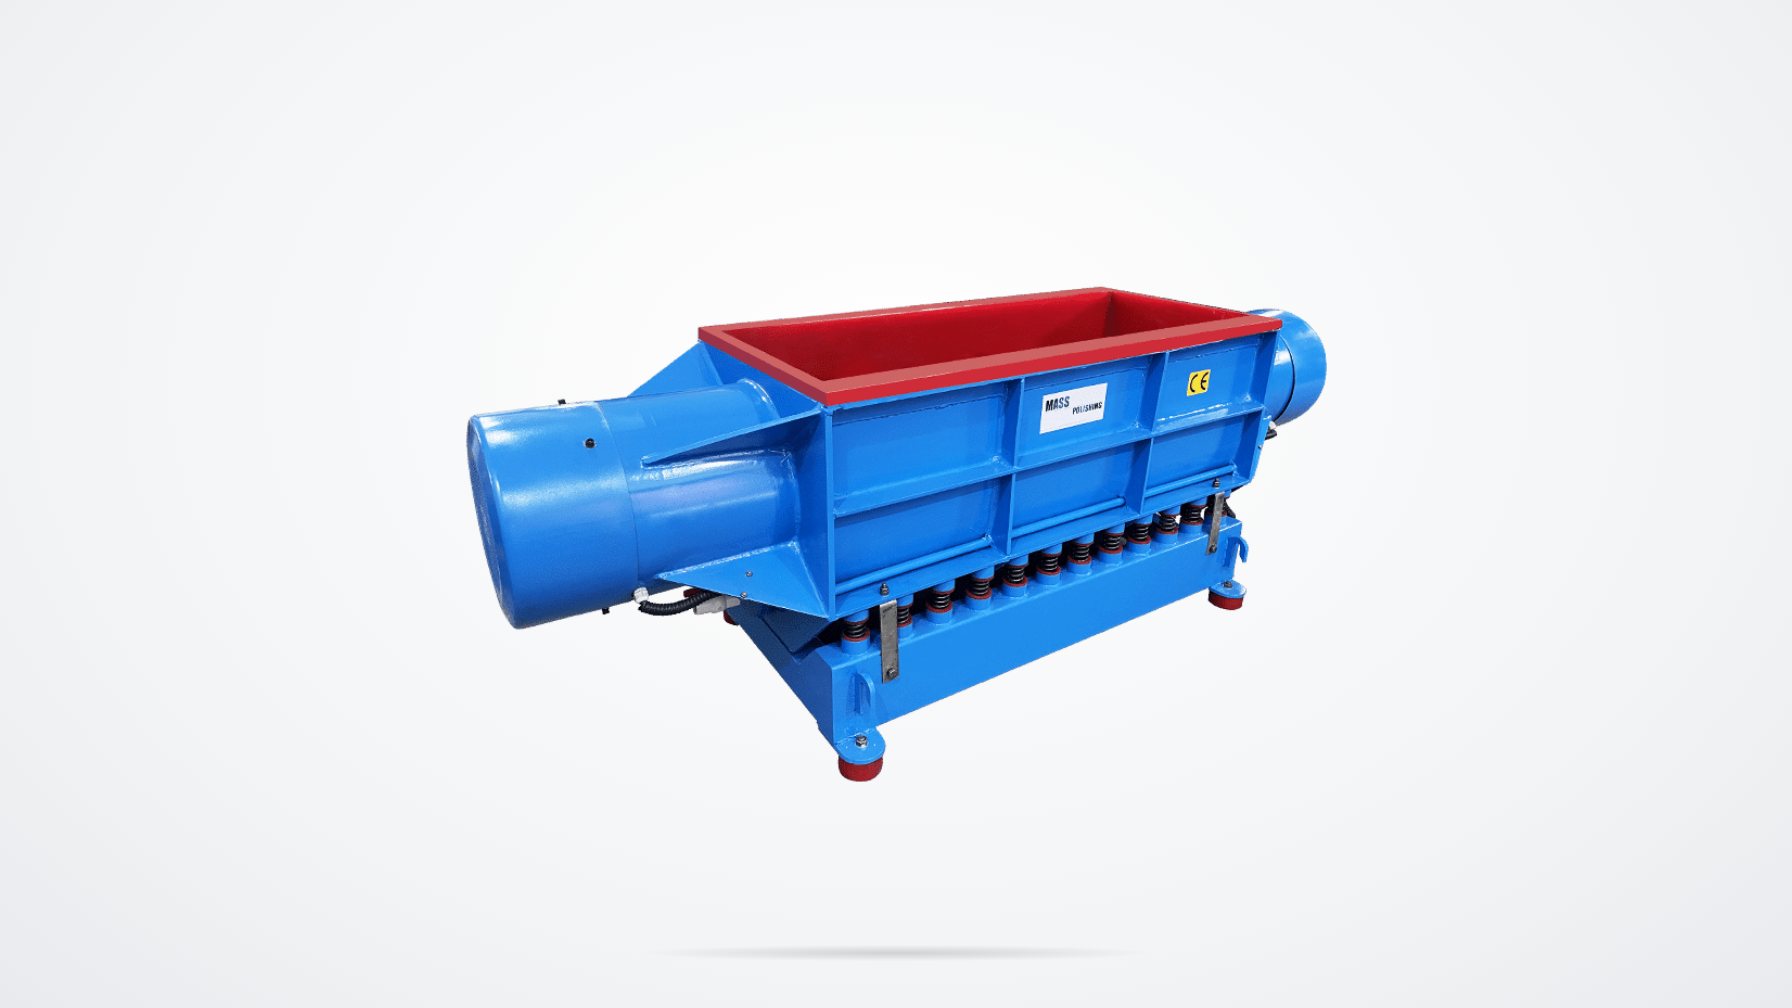
Close-tolerance features change the decision. A threaded hole in a turned steel fitting cannot be processed like an outside edge. Media small enough to reach the thread root can also round the crest if the cycle runs too long. I would rather run two short cycles and inspect the thread than run one long cycle and hope. For thin-wall parts, part-on-part contact tends to produce dents before it removes burrs. A specials divider in a vibratory bowl or a tub machine with chamber dividers keeps workpieces separate.
How do you deburr a threaded or reamed hole without changing the tolerance
Choose media that fits the smallest opening and keep the energy below the point where crests begin to wash. Stop when the burr root is gone, not when every tool mark disappears. For reamed holes, this usually means checking the part at half the expected cycle time and adjusting from there, because thread and bore size change far faster than an outside edge.
What protects thin-wall turned parts from distortion during steel deburring
Divided chambers or custom fixtures stop parts from striking each other. We specify specials dividers in vibratory bowls when each part must move independently. For long thin stems and shafts, a tub vibrator spaces the load better than a round bowl, and reduced speed through a VFD makes the process gentler without losing the deburring effect.
Part Sample Processing Before Deburring Equipment Commitment
Most steel machining deburring mistakes are visible only after a process is locked. Mass Polishing removes that risk by running sample parts on the intended machine, with the intended media and compound, before any equipment or contract finishing decision. Send the part number, material, heat treat condition, and monthly quantity to [email protected] or call +86 572 000 0000. We document the resulting edge break, surface finish, and cycle time so the quoted process is not a guess.
Common Questions About Steel Machining Deburring
Can one machine deburr both milled and turned steel parts
Yes, if the part envelope and burr roots are similar. A vibratory bowl with the correct ceramic media handles mixed machined parts well because the process does not care whether a burr came from milling or turning. It responds to part mass, media pressure, and cycle time. The exception is a family of parts with very different risk profiles, such as heavy milled brackets next to thin turned shafts. In that situation, separate programs, dividers, or a second machine reduce the chance of damaging the more delicate part while chasing the heavier burr.
Is vibratory deburring aggressive enough for hard turned steel
cURL Too many subrequests by single Worker invocation. To configure this limit, refer to https://developers.cloudflare.com/workers/wrangler/configuration/#limits.
cURL Too many subrequests by single Worker invocation. To configure this limit, refer to https://developers.cloudflare.com/workers/wrangler/configuration/#limits
cURL Too many subrequests by single Worker invocation. To configure this limit, refer to https://developers.cloudflare.com/workers/wrangler/configuration/#limits.
cURL Too many subrequests by single Worker invocation. To configure this limit, refer to https://developers.cloudflare.com/workers/wrangler/configuration/#limits
cURL Too many subrequests by single Worker invocation. To configure this limit, refer to https://developers.cloudflare.com/workers/wrangler/configuration/#limits.
Si vous êtes intéressé, consultez ces articles liés :
Démarrer avec la finition de masse : un guide complet
cURL Too many subrequests by single Worker invocation. To configure this limit, refer to https://developers.cloudflare.com/workers/wrangler/configuration/#limits